Technology / LPBF / Materials
/ LPBF · Laser Powder Bed Fusion Materials portfolio

Seven validated
LPBF powders
for the Z Rapid iSLM series.

Aluminium, stainless steel, tool steel, titanium, nickel, cobalt-chrome and chromium bronze, each with process parameters validated by Z Rapid. All powders are spherical and 15–53 µm (titanium 15–45 µm).

7 alloys. AlSi10Mg, 316L, MS1, TC4, IN718, MP1 and QCr1, from prototype to series.
High density. Relative density ≥ 99% for most alloys, up to ≥ 99.9% for titanium.
Measured properties. Tensile strength, yield strength, elongation and hardness per alloy are listed in the table below.
3DPS BENELUX supply chain. Powder sourcing, certificates and lifecycle tracking — we handle the complete powder logistics for your production.
AlAluminium
FeSteel
TiTitanium
NiNickel
CoCobalt
CuCopper
Grain structure per family
[ 01 · Properties ]

Material properties

The seven standard powders for Z Rapid LPBF systems, with the key mechanical properties from the manufacturer's datasheets.

Alloy Rel. density Tensile strength Rm (MPa) Yield strength Rp0.2 (MPa) Elongation A Hardness Density (g/cm³)
AlSi10MgAluminium alloy ≥ 95% ≥ 330 ≥ 245 6% 120 HB 2.67
316LStainless steel · 1.4404 ≥ 99% ≥ 560 ≥ 480 10–20% 158 HB 7.89
MS1Maraging tool steel ≥ 99% ≥ 1090 ≥ 1000 10% (4%*) 323 HB 8.0
TC4Ti6Al4V · titanium ≥ 99.9% ≥ 1000 ≥ 900 4–10% 294 HB 4.51
IN718Nickel superalloy ≥ 99% ≥ 980 (1240*) ≥ 700 (1000*) 12–30% 283 HB (455*) 8.15
MP1Cobalt-chrome · CoCrMoW ≥ 99% ≥ 1000 ≥ 900 10% 323–428 HB –
QCr1Chromium bronze · CuCr1 ≥ 98% 300 200 5% 170–200 HB 8.9

As-built values according to the Z Rapid datasheets. * After heat treatment. Indicative values: actual properties depend on build orientation, parameters and post-processing. Powders: spherical, 15–53 µm (TC4: 15–45 µm). Full datasheets with chemical composition on request.

[ 02 · Datasheets ]

Datasheet per alloy

Powder, chemical composition and printed properties per alloy, with an example part printed on a Z Rapid LPBF system.

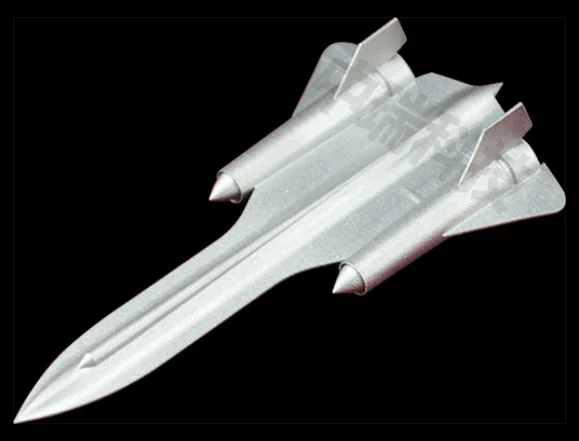
Aircraft model in AlSi10Mg, printed with LPBF
Grain structure
/ 01 · Aluminium

AlSi10Mg

Light, thermally conductive and fast to print. For lightweight housings, brackets, heat exchangers and functional prototypes.

Automotive · Aerospace · Thermal
Powder
Particle size15–53 µm
ShapeSpherical
Flowability (Hall)150 s
Apparent density1.45 g/cm³
Chemical composition (%)
Al balanceSi 9–10Mg 0.2–0.45Cu ≤ 0.05Mn ≤ 0.45Ni ≤ 0.05Fe ≤ 0.55Ti ≤ 0.15O ≤ 0.15
Printed properties (as-built)
Relative density≥ 95%
Density2.67 g/cm³
Tensile strength Rm≥ 330 MPa
Yield strength Rp0.2≥ 245 MPa
Elongation at break6%
Elastic modulus70 GPa
Hardness120 HB
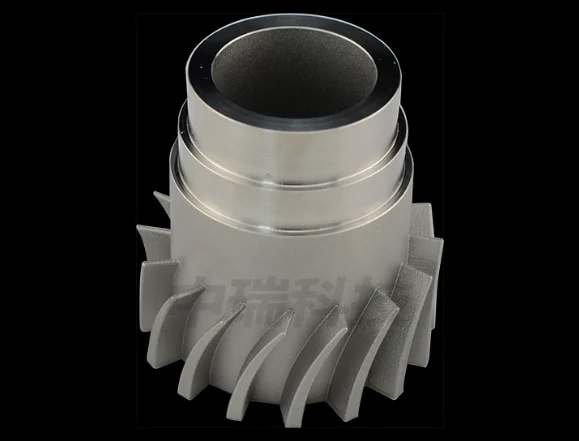
Impeller in 316L, printed with LPBF
Grain structure
/ 02 · Stainless steel

316L

Corrosion resistant and tough: the workhorse for functional parts, fluid handling, food and marine applications.

Manufacturing · Food · Marine
Powder
Particle size15–53 µm
ShapeSpherical
Flowability (Hall)40 s
Apparent density3.9 g/cm³
Chemical composition (%)
Fe balanceCr 16–18Ni 10–14Mo 2–3Mn ≤ 2Si ≤ 1C ≤ 0.03P ≤ 0.045S ≤ 0.03O ≤ 0.13H ≤ 120 ppm
Printed properties (as-built)
Relative density≥ 99%
Density7.89 g/cm³
Tensile strength Rm≥ 560 MPa
Yield strength Rp0.2≥ 480 MPa
Elongation at break10–20%
Elastic modulus180 GPa
Hardness158 HB
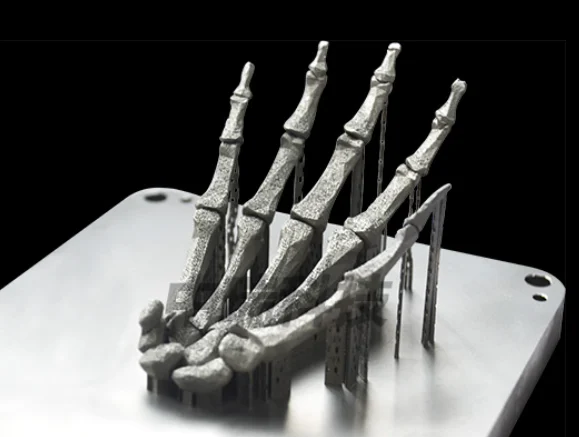
Hand skeleton in MS1 on the build plate, printed with LPBF
Grain structure
/ 03 · Tool steel

MS1

Maraging steel for mould inserts and tooling, including conformal cooling channels. Hardness increases strongly after ageing.

Tooling · Moulds
Powder
Particle size15–53 µm
ShapeSpherical
Flowability (Hall)40 s
Apparent density4.3 g/cm³
Chemical composition (%)
Fe balanceNi 17–19Co 8.5–9.5Mo 4.2–5.2Ti 0.8–0.9Al 0.05–0.15Mn ≤ 0.1C ≤ 0.03S ≤ 0.01O ≤ 0.15
Printed properties (as-built)
Relative density≥ 99%
Density8.0 g/cm³
Tensile strength Rm≥ 1090 MPa
Yield strength Rp0.2≥ 1000 MPa
Elongation at break10% (4% after HT)
Elastic modulus160 GPa (180 after HT)
Hardness323 HB
Cut-away housings in titanium TC4, printed with LPBF
Grain structure
/ 04 · Titanium

TC4 · Ti6Al4V

Highest strength-to-weight ratio and biocompatible. For aerospace structures, motorsport and medical applications.

Aerospace · Medical · Motorsport
Powder
Particle size15–45 µm
ShapeSpherical
Flowability (Hall)45 s
Apparent density2.5 g/cm³
Chemical composition (%)
Ti balanceAl 5–6.75V 3.5–4.5Fe ≤ 0.3C ≤ 0.1Si ≤ 0.12O ≤ 1300 ppmN ≤ 400 ppmH ≤ 120 ppm
Printed properties (as-built)
Relative density≥ 99.9%
Density4.51 g/cm³
Tensile strength Rm≥ 1000 MPa
Yield strength Rp0.2≥ 900 MPa
Elongation at break4–10%
Elastic modulus100–120 GPa
Hardness294 HB
Perforated ring in IN718, printed with LPBF
Grain structure
/ 05 · Nickel

IN718

Retains strength at high temperature. For hot-section parts in turbines, rocket propulsion and energy.

Aerospace · Energy · Space
Powder
Particle size15–53 µm
ShapeSpherical
Flowability (Hall)45 s
Apparent density4.4 g/cm³
Chemical composition (%)
Ni 50–55Fe balanceCr 17–22Nb 4.75–5.5Mo 2.8–3.3Ti 0.65–1.15Al 0.2–0.8Co ≤ 1Si ≤ 0.35C ≤ 0.08P ≤ 0.015
Printed properties (as-built)
Relative density≥ 99%
Density8.15 g/cm³
Tensile strength Rm≥ 980 MPa (1240 after HT)
Yield strength Rp0.2≥ 700 MPa (1000 after HT)
Elongation at break12–30%
Elastic modulus140–180 GPa
Hardness283 HB (455 after HT)
Dental crowns in cobalt-chrome on the build plate
Grain structure
/ 06 · Cobalt-chrome

MP1 · CoCr

Biocompatible, hard and wear resistant. The standard for dental crowns and bridges, in large numbers per build plate.

Dental · Medical
Powder
Particle size15–53 µm
ShapeSpherical
Flowability (Hall)45 s
Apparent density4.2 g/cm³
Chemical composition (%)
Co balanceCr 22–23Mo 5–10W 5–10Si ≤ 1.5C ≤ 0.03O ≤ 0.13
Printed properties (as-built)
Relative density≥ 99%
Densitynot specified
Tensile strength Rm≥ 1000 MPa
Yield strength Rp0.2≥ 900 MPa
Elongation at break10%
Elastic modulus200 GPa
Hardness323–428 HB
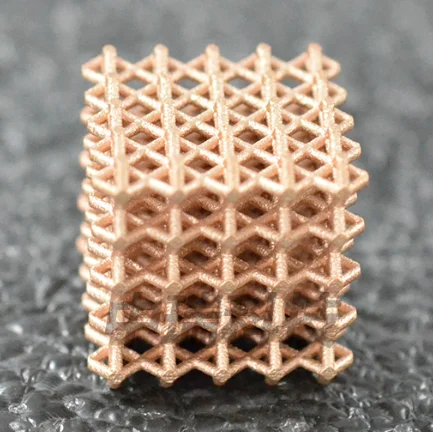
Lattice structure in chromium bronze QCr1, printed with LPBF
Grain structure
/ 07 · Copper

QCr1 · chromium bronze

Copper alloy with good thermal and electrical conductivity. For heat exchangers, heat sinks, inductors and lattice structures.

Electrical · Thermal
Powder
Particle size15–53 µm
ShapeSpherical
Flowability (Hall)50 s
Apparent density4.8 g/cm³
Chemical composition (%)
Cu balanceCr 0.5–1.5Zr 0.04–0.1Mg 0.04–0.08
Printed properties (as-built)
Relative density≥ 98%
Density8.9 g/cm³
Tensile strength Rm300 MPa
Yield strength Rp0.2200 MPa
Elongation at break5%
Elastic modulus90 GPa
Hardness170–200 HB
Need a different material? Z Rapid systems also run other commercial metal powders. We assess per project what is feasible and which validation is needed. Ask your question →

* HT = heat treatment. Values according to the Z Rapid datasheets; indicative, depending on build orientation, parameters and post-processing. MS1: the datasheet lists 8.5–9.5% chromium; for maraging steel this is cobalt (Co). 316L: phosphorus corrected to ≤ 0.045%. MP1: density not correctly stated in the datasheet.

The images show an illustrative rendering of the typical grain structure, in the style of a colour-etched micrograph. They are not measurements of these specific parts.

[ 03 · 3DPS · End-to-end ]

What 3DPS does around LPBF materials

/ Selection

Alloy advice

Based on your part requirements — load case, environment, certification — we advise which alloy(s) are feasible. Including comparison with the conventional production route.

/ Sourcing

Powder & certificates

Gas-atomized powder from OEM-validated suppliers, with material certificates (3.1 / 3.2). Powder lifecycle tracking and lot traceability for audit trail.

/ Qualification

Custom parameter sets

For non-standard alloys or modified process requirements: feasibility process with test builds, parameter optimization and mechanical characterization — your IP, your parameters.

/ Production

Build & post-processing

Production on LPBF systems plus the complete post-processing chain: stress relief, support removal, HIP (where needed), heat treatment, surface finishing and CMM inspection.

[ 04 · Scope & caveats ]

What we can produce — and what we first establish together

The alloys above give an honest picture of LPBF possibilities. Which of them work in practice for your part depends on geometry, requirements and certification. This overview makes explicit what is standard and what requires a feasibility process — so expectations stay aligned.

Standard within our LPBF capability

  • Three Z Rapid platforms: iSLM160, iSLM280 and iSLM300D, selected on build volume and series size.
  • The seven alloys above with process parameters validated by Z Rapid.
  • Complete post-processing chain: stress relief, support removal, HIP, heat treatment, surface finishing, CMM.
  • 3.1/3.2 material certificates and powder lot traceability for audit-trail parts.

To establish per project

  • Mechanical properties vary with laser power, layer thickness, build orientation and post-process. Datasheet values are reference figures, not contractual.
  • Availability per model: not every alloy is validated on every iSLM model. We confirm this per project.
  • Custom alloys or modified parameter sets require a feasibility process with test builds and mechanical characterization.
  • Industry-specific certification (medical, aerospace, defense) — contact us early so the production route can be tuned accordingly.
[ Next step ]

Which alloy fits your part?

Send a drawing or description of a typical part from your production, with the relevant requirements (load, temperature, environment, certification). Within five working days you'll receive a substantiated material recommendation — including alternatives and, if appropriate, an invitation for a live print benchmark in our BENELUX demo space.

Send us a WhatsApp