Eleven validated applications
in Wire-Laser DED.
Concrete parts printed on Meltio Wire-Laser machines — with dimensions, material, weight and print time. No renderings, no marketing mock-ups: industrial parts from the Meltio ecosystem that are in production or recently delivered. Filter by your sector to find relevant examples.
Applications selected from the global Meltio ecosystem. We only show parts that are representative of BENELUX industry. Local reference installations and case studies of 3DPS customers in preparation — ask for BENELUX-specific references during your strategy call.

Engine bracket
Structural engine bracket in stainless steel for aviation. Printed near-net-shape, followed by CNC for the mounting features. Replaces a part milled from billet with considerable material savings.

Propulsion adapter
Propulsion adapter in titanium Grade 5 for an unmanned aerial system. A lightweight application where the high strength-to-weight ratio of Ti6Al4V is decisive. Near-net-shape printing saves 60–70% material compared to billet machining.
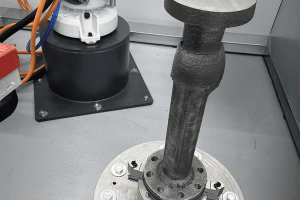
Eductor for marine systems
On-demand production of an eductor for ship systems — a classic defence spare-part application where the OEM supply chain is too slow. Printed locally in days instead of weeks through official channels, in the same or an improved alloy.
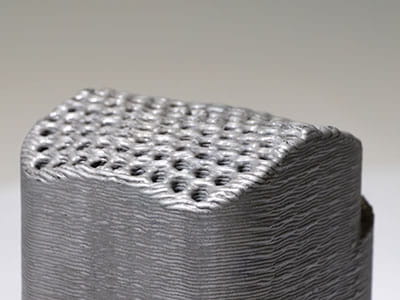
Anti-cavitation valve
Process valve with internal geometry for flow conditioning and cavitation suppression. Wire-laser deposits the rough profile, followed by CNC for the seal grooves and critical inner diameters. Replaces a cast part with a 12-week lead time.

300 mm diffuser · legacy spare
Custom 300 mm diffuser for a process installation whose OEM has left the market. Reverse-engineered from a worn original, then printed and certified for return to service. No casting tooling needed, no import dependency.
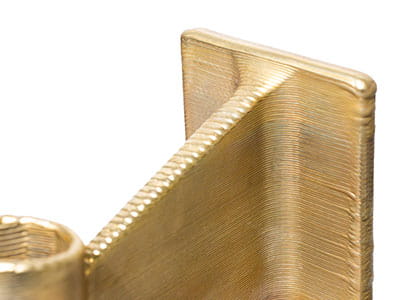
Boat-shaft bracket
Shaft bearing bracket in marine bronze for shipbuilding — corrosion-resistant in salt water, high mechanical strength. A classic wire-laser application: medium-sized geometry, dense structure, casting not economical for one-offs.
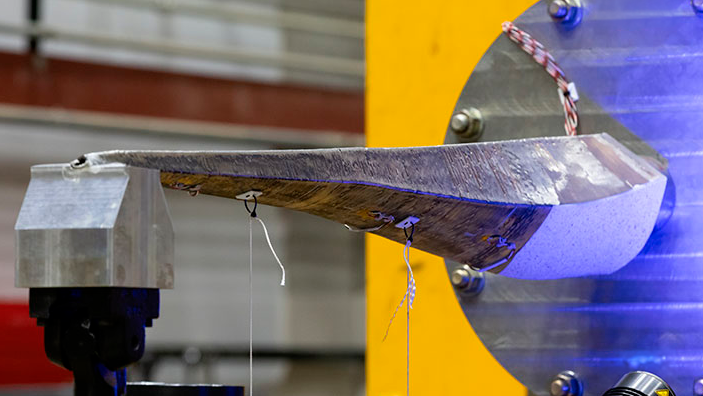
Tidal turbine spar
Structural spar for a tidal turbine in the marine energy sector. Robust geometry, high fatigue loading, long service life in an aggressive maritime environment. Wire-laser DED enables design freedom that is not economical conventionally.

Heat exchanger · CuCrZr
Heat exchanger in copper-chromium-zirconium for high thermal conductivity. Used in the research and energy sectors where both thermal conductivity and mechanical strength are required. Demonstrates the Blue Laser advantage: copper absorption that IR cannot achieve.
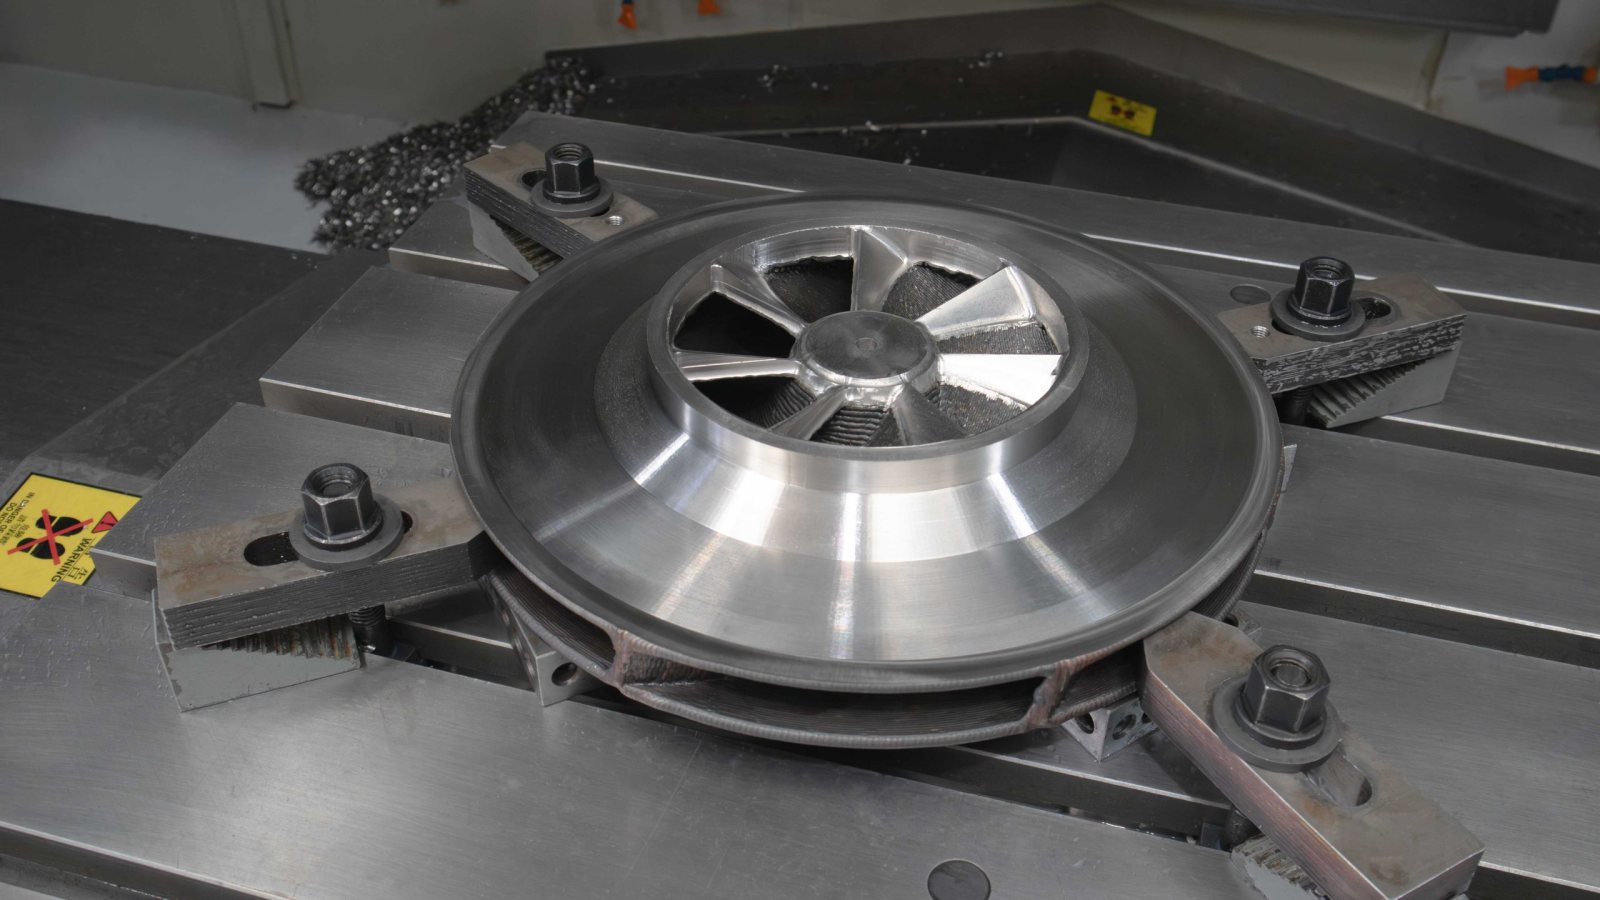
Closed impeller · fire suppression system
Pump impeller for a fire suppression system in critical infrastructure. Geometry traditionally cast with a long lead time; wire-laser deposits near-net-shape with direct CNC finishing. Lead time reduced from weeks to days for mission-critical spares.
Stub axle · race car
Axles for the motorsport sector, where weight saving and custom geometry go hand in hand. A multi-material application with wire switching: high-strength steel in critical zones, lighter material where the load allows.
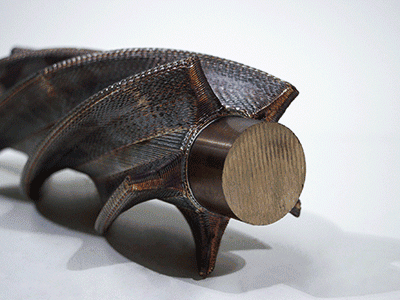
Screw compressor · cladding
Worn screw compressor from heavy mining equipment, restored with wire-laser cladding on the wear zones. Result: an improved service life compared to the original — not just a repair but an on-site upgrade.
No applications match this filter.
Four rules of thumb for Wire-Laser DED.
Not every part belongs on a Wire-Laser DED machine. Below are the criteria that predict whether it will pay off — derived from Meltio's global validation library and our own BENELUX projects. For parts that do not meet these criteria, LPBF may be a better route.
- Medium to very large Sweet spot > 100 mm to 1 m+. Below 100 mm powder bed often wins on precision; above 1 m+ a robotic or gantry configuration becomes attractive.
- Hybrid: adding to existing geometry Repair, cladding, feature addition on shafts or flanges — applications where a part already exists and material is only added locally. Powder bed fundamentally cannot do this.
- Expensive or hard-to-machine materials Titanium, Inconel, tool steel — alloys with a high buy-to-fly ratio in conventional billet machining. The material savings of near-net-shape translate directly into ROI.
- Moderate geometric complexity Suitable for parts that would traditionally be cast or forged, with a minimum wall thickness above 2 mm. For lattice structures or fine internal channels, powder bed remains the right route.
A part that could have been on this list?
Send us a drawing, description or photo. Within 5 working days you receive a substantiated assessment: whether wire or powder fits, material, lead time, and honest "don't do it" advice if AM offers no gain in this case.